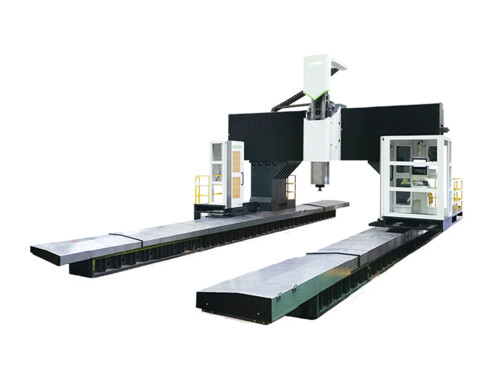
Wind turbine hubs are large, heavy components with multiple mounting faces, large bores, and complex bolt-hole patterns. When you machine them, you need a CNC machine that can handle the workpiece size and weight while maintaining stability and accuracy throughout the process.
When choosing a CNC machine for wind turbine hub machining, you should look beyond table size and spindle speed. You need to match the machine to the hub’s dimensions, weight, machining faces, bore size, hole patterns, cutting requirements, and number of setups. This guide explains the key factors you should check before selecting a machine.
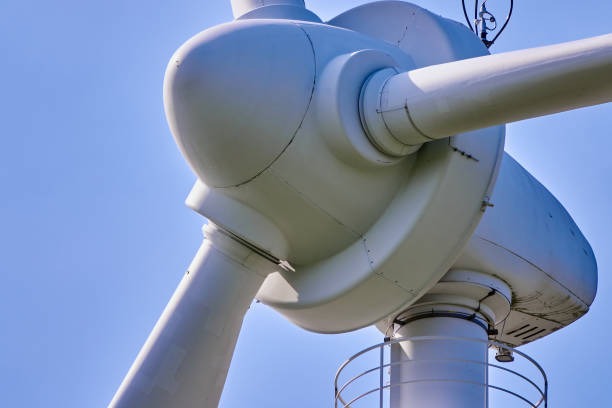
A wind turbine hub is the central component that connects the turbine blades to the main shaft. It transfers the rotational force from the blades to the drivetrain and supports the loads generated during operation.
For machining, you can think of the hub as a large, heavy, multi-face component. Its key features typically include blade mounting areas, large bores, bolt holes, and other locating surfaces that require accurate positioning. These features directly affect the CNC machine configuration you need.
The hub connects the blades to the turbine’s main shaft and transfers the forces generated by the rotating blades. Because it carries significant loads, its mounting and locating surfaces need to be machined accurately.
The hub’s large size, weight, and multiple machining surfaces make machine selection important. You need enough table capacity, travel, rigidity, and machining capability to complete the required operations without unnecessary setups.
Wind turbine hub machining involves several factors that directly affect your CNC machine selection.
You should select the CNC machine based on the hub size, weight, geometry, machining operations, and required accuracy, rather than looking at a single machine specification.
You can use different CNC machine configurations for wind turbine hub machining. Your choice should depend on the hub size, weight, machining surfaces, feature geometry, and number of setups.
|
CNC Machine Type |
Suitable For |
Key Considerations |
|
VMC |
Small to medium-sized hubs and mainly vertical machining operations |
Check table size, load capacity, X/Y/Z travel, and spindle torque. |
|
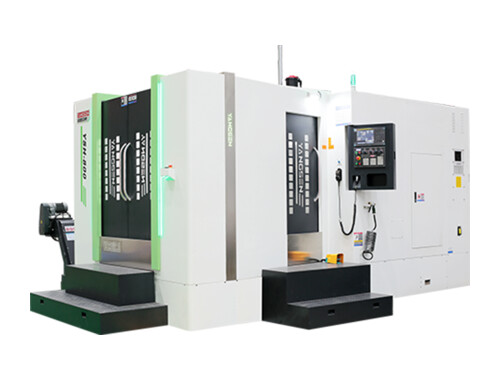
HMC |
Hubs requiring machining on multiple sides |
Useful when you need better access to multiple faces and fewer setups. Check rotary indexing, pallet size, and spindle torque. |
|
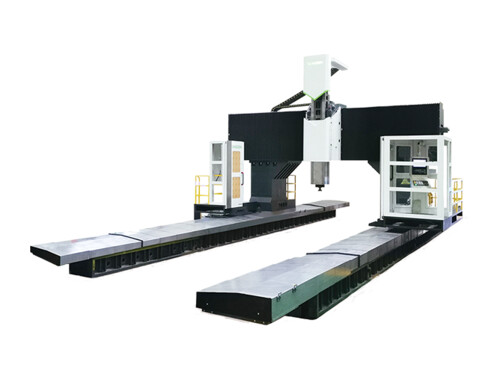
Gantry Machining Center |
Large and heavy hubs |
Check table dimensions, maximum workpiece weight, gantry clearance, travel, rigidity, and spindle power. |
|
5-Axis Machining Center |
Hubs with complex surfaces, angled features, or multiple machining orientations |
Useful when you need to reach multiple features with fewer setups. Check rotary-axis capacity, accuracy, and work envelope. |
The machine you choose should match the actual hub dimensions and machining process, not simply the largest available machine.
When you choose a CNC machine for wind turbine hub machining, you need to look beyond the basic machine size. Check these eight factors against your actual hub dimensions, machining operations, and production requirements.
Check the hub’s maximum diameter, height, and overall dimensions first. Your machine needs enough working space for the hub, fixture, cutting tools, and tool movement without restricting access to the machining area.
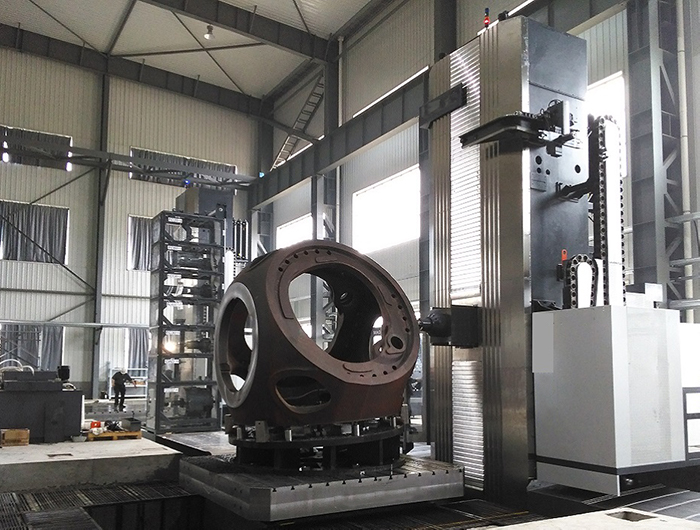
Check the total weight of the hub and fixture together. Make sure the table load capacity is sufficient for the complete setup and leaves a reasonable safety margin for stable machining.
Compare the hub dimensions with the machine’s X, Y, and Z travel. You need enough travel to reach all required machining areas without forcing the tool or workpiece into an unsuitable position.
Wind turbine hubs can require heavy roughing and large-diameter boring. Check spindle power and torque, especially at the cutting speeds you actually plan to use. Maximum RPM alone does not tell you whether the spindle is suitable.
If you need to machine multiple faces or bolt-hole patterns, consider the rotary axis carefully. Check its load capacity, indexing accuracy, and repeatability to make sure it can handle the hub and maintain the required positioning.
Large hubs and heavy cutting operations can generate high cutting forces. A rigid machine helps you control vibration and maintain stable cutting conditions during roughing, boring, and milling.
Large hubs can involve long cutting cycles and significant material removal. You should check the machine’s coolant flow, chip conveyor, and chip evacuation design to prevent chips from building up around the workpiece and cutting area.
Think about how many times you need to reposition the hub. If you can complete more operations in fewer setups, you can reduce setup time and minimize the positioning errors that may occur when the workpiece is moved.
You should choose the CNC machine based on the actual hub requirements, not simply by selecting the largest machine available. Start with the hub size and weight, then consider the machining faces, feature geometry, required accuracy, and number of setups.
|
Wind Turbine Hub Requirement |
CNC Machine to Consider |
Why |
|
Small or medium hub with mainly vertical operations |
VMC |
Suitable for drilling, milling, and boring when most features are accessible from one main direction. |
|
Multiple machining faces and frequent indexing |
HMC |
Gives you better access to different faces and can reduce workpiece repositioning. |
|
Large and heavy hub |
Gantry Machining Center |
Provides a larger working envelope, higher table capacity, and the rigidity needed for heavy machining. |
|
Complex angles or difficult-to-access features |
5-Axis Machining Center |
Allows you to reach multiple surfaces and features with fewer setups. |
|
Large hub with heavy roughing and boring |
Heavy-duty HMC or Gantry |
You need sufficient spindle torque, rigidity, travel, and load capacity for high cutting forces. |
|
Hub requiring high positional accuracy between multiple features |
HMC, Gantry, or 5-Axis |
The right configuration can reduce repositioning and help maintain feature-to-feature accuracy. |
When two machine types can meet your requirements, compare the number of setups, machining time, fixture requirements, and total process cost. You do not necessarily need more axes or a larger machine if your hub can be machined efficiently with a simpler configuration.
Before you buy a CNC machine for wind turbine hub machining, compare the specifications that directly affect your workpiece and machining process. Do not focus only on spindle speed or machine size.
|
Specification |
What You Should Check |
|
X/Y/Z Travel |
Make sure the available travel covers the hub and all required machining positions. |
|
Table Size |
Check whether the hub and fixture can fit with enough working clearance. |
|
Table Load Capacity |
Confirm that the machine can safely support the hub, fixture, and other setup components. |
|
Spindle Power |
Check whether the spindle can handle your roughing, milling, and boring requirements. |
|
Spindle Torque |
Important for heavy cutting and large-diameter boring operations. |
|
Spindle Taper |
Match the taper and tooling system with the cutting tools you plan to use. |
|
Rotary Table |
Check diameter, load capacity, indexing accuracy, and repeatability if rotary machining is required. |
|
Positioning Accuracy |
Make sure the machine can meet the required positioning tolerance for critical hub features. |
|
Repeatability |
Important when you need consistent results across multiple machining operations or parts. |
|
Tool Capacity |
Make sure the ATC has enough tool positions for drilling, milling, boring, and other operations. |
|
Coolant System |
Check coolant flow, pressure, and delivery for long cutting cycles and heavy material removal. |
|
Chip Removal |
Check whether the chip conveyor and machine design can handle the expected chip volume. |
You should also ask the machine supplier to confirm these specifications under the actual configuration you plan to purchase, especially when the machine includes a large rotary table, extended travel, or other options that can affect its working capacity.
Setup time can become a major part of the machining cycle when you need to reposition a large and heavy hub several times. You can reduce it by choosing the right machine configuration and planning the machining process around fewer setups.
Choose a machine configuration that gives you access to multiple machining faces without moving the hub unnecessarily. An HMC or 5-axis machine can be useful when several features need to be machined from different directions.
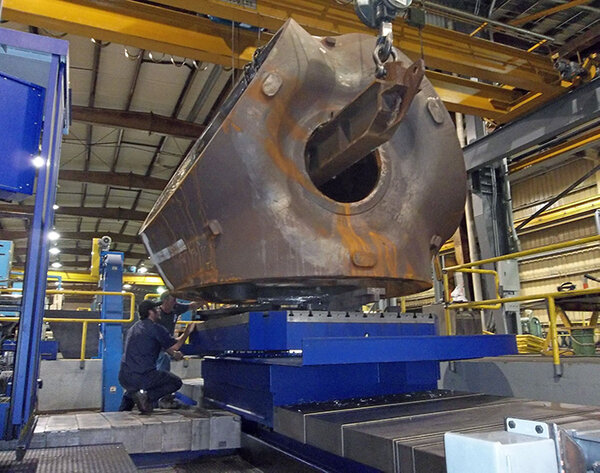
A rotary table can help you index the hub to different machining positions without removing it from the fixture. Before choosing one, check its load capacity, table diameter, indexing accuracy, and available working space.
Try to complete related operations in the same setup. Combining drilling, milling, and boring can reduce the number of times you need to remove and reposition the hub.
Every repositioning adds setup time and creates another opportunity for positioning errors. Plan the machining sequence so that you can complete as many critical features as possible before moving the workpiece.
A probing system can help you verify workpiece position and locate critical features before machining. This can reduce manual measurement and help you detect setup errors before they affect the part.
Q: What type of CNC machine is best for wind turbine hub machining?
A: There is no single machine type for every wind turbine hub. You should choose between a VMC, HMC, gantry machining center, or 5-axis machine based on the hub’s size, weight, geometry, machining faces, and required setups.
Q: Is an HMC better than a VMC for large wind turbine hubs?
A: An HMC can be useful when you need to machine multiple sides of the hub. Its horizontal spindle configuration can provide better access to different faces and help reduce repositioning. However, you should compare the actual machining process rather than choosing based on machine type alone.
Q: When is a gantry machining center required for wind turbine hub machining?
A: A gantry machining center becomes a practical option when the hub is too large or heavy for a conventional machining center. Check the required table size, load capacity, gantry clearance, travel, spindle torque, and machine rigidity.
Q: What spindle power is needed for wind turbine hub machining?
A: The required spindle power depends on the material, cutting tools, cutting depth, feed rate, and roughing strategy. Instead of selecting a machine based on spindle power alone, you should calculate the cutting requirements for your actual hub and check both spindle power and torque.
Q: How important is rotary table accuracy for wind turbine hub machining?
A: It is important when you use rotary indexing to machine multiple faces or bolt-hole patterns. You should check indexing accuracy, repeatability, load capacity, and table diameter to make sure the rotary axis matches your machining requirements.
Q: What information should I provide when selecting a CNC machine for a wind turbine hub?
A: Provide the supplier with the hub’s dimensions, weight, material, drawings, critical tolerances, bore sizes, hole patterns, required machining operations, production volume, and preferred tooling. This gives the supplier enough information to recommend a suitable machine configuration rather than quoting a machine based only on workpiece size.
Choosing a CNC machine for wind turbine hub machining starts with the part, not the machine. You need to consider the hub’s size, weight, machining faces, bore and hole requirements, cutting conditions, accuracy, and number of setups.
Once you define these requirements, you can compare VMCs, HMCs, gantry machining centers, and 5-axis machines based on their actual capabilities.
Need help selecting a CNC machine for your wind turbine hub? Share your hub drawing, dimensions, weight, and machining requirements with our engineers. We can help you evaluate the required machine configuration and key specifications.
STICHWORTE :